圣鑫管业

06

2026

-

10

Uneven cup rim—making the lid hard to screw on? How a common flaw can ruin the user experience.


Author:

A customer sent a photo: a coffee stain on the cuff of a white shirt. The accompanying caption reads, “Your lid doesn’t work—it leaks.”

This complaint is something cup manufacturers hear dozens of times a year. It sounds perfectly reasonable—since the liquid is leaking from the lid, it must be the lid’s fault. But is it really the lid’s fault?
01. The leakage point is actually at the “joint.”

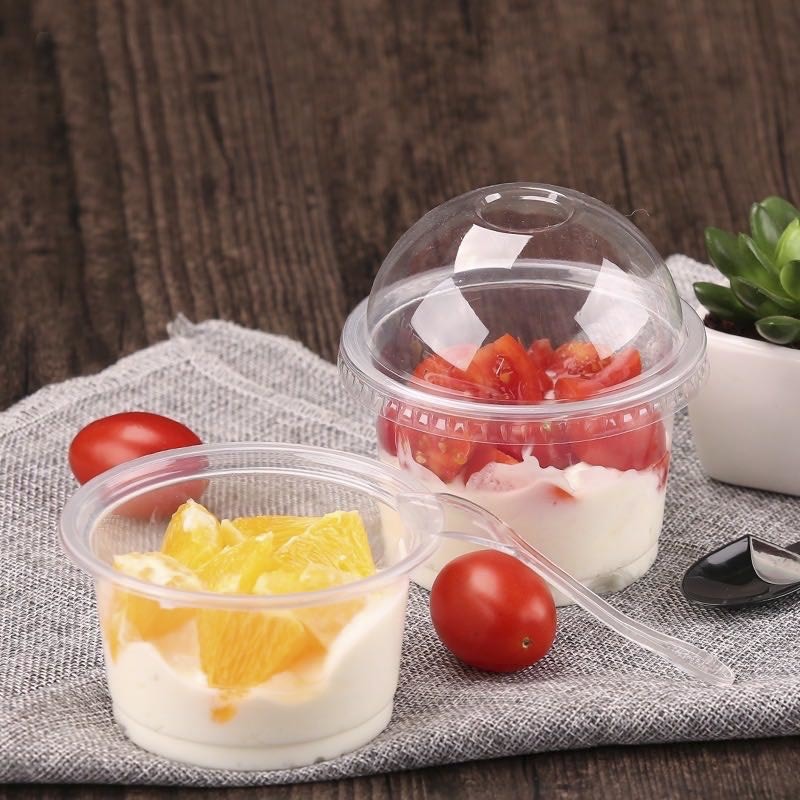
Let’s start with a phenomenon: if you hold a sealed cold drink cup at an angle for a while, the liquid will begin to spill out… The ring where the outer edge of the lid snaps into the curled rim of the cup. It seeps through, leaving a small ring of water on the tabletop. Factories that produce mugs have almost all encountered this kind of issue.
The problem lies in the phrase “continuous seal.” When the cup is tilted, the liquid is forced against the cup’s walls. At that point, if there is a complete seal between the rim and the lid, the liquid cannot escape; but as soon as this seal is broken anywhere, the gap becomes the only path for the liquid to flow out.
On the other hand, The key is never whether the lid fits tightly, but rather whether the sealing surface around the cup rim and the lid forms an airtight seal.
The customer receives exactly this cup. Whether it leaks or not, they won’t know while they’re still in the shop.

02. 0.5 millimeters—enough to shatter a cup.

The cup holder is not an exterior part; it is… Functional component In the packaging industry, this type of fit is known as an “interference fit”—the inner diameter of the lid is slightly smaller than the cup’s opening, and when the lid is snapped on, the material’s inherent elasticity creates a tight seal.

    \\        0.5 mm

With such a large difference in the cup’s mouth diameter, even the tightest-fitting lid will pop off.

How sensitive is it? The packaging plant’s empirical data show: Even a difference of just 0.5 millimeter in the cup’s mouth diameter, or a slight variation in the latch height, is enough to cause a lid that appears tightly sealed to pop open under minimal pressure.
What does 0.5 millimeter mean? Roughly, it’s about the thickness of a business card. And the precision of the cup’s rim is set in one go during the thermoforming process— The moment the cup comes off the machine, whether it will leak is pretty much sealed.

03. Root Cause One: Sheet Thickness and Heating Temperature

The cup rim curl has developed a problem; the root cause usually lies in three areas: Heating temperature profile, mold gap, sheet thickness tolerance . Let’s start with temperature and sheet material, which are often the most easily overlooked.
When a cup-making machine forms PP cups, the temperature of the sheet material is not uniform across the entire surface; rather, it is… Two distinct numbers: the center and the edge. :       
Sheet center: 170–185°C —— The temperature must be sufficient to allow the material to be drawn; otherwise, the cup bottom is prone to becoming too thin, developing holes, or cracking. Sheet edge 155–165℃ —— The temperature must be controlled, as the cup rim needs to maintain its rigidity.
Why does the cup rim need to be kept at a low temperature? Because the rim is formed by rolling, and if the edge is too soft, Stretching, ovalization, and flanging deformations will all be produced. In the industry, this process is described as having “extremely low tolerance for error”: if the core temperature is insufficient, it will crack; if it’s too high, it will wrinkle; and… When the edge temperature rises, deformation of the mouth is inevitable. 。       
The thickness tolerance of the sheet material itself also serves as the starting point for cup‑mouth precision.
PP material is particularly difficult to work with. Its processing window is inherently narrow, Fluctuations of ±5℃ This alone is enough to cause shrinkage deformation, poor stretching, and dimensional deviations. If the ambient temperature differs by 5 degrees between morning and afternoon and you make no adjustments, the resulting cup rim may end up being a different size.

04. Root Cause No. 2: Molds Age

Molds do wear out. Over time, The rim of the cup will have burrs and uneven thickness. , it requires regular polishing and calibration. Once this process is delayed, product consistency begins to deteriorate—gradually and in ways that are difficult to detect.
In addition to the wear, there are several specific pieces of physical evidence:
Flash · Burring · Sink Marks · Mold Line Misalignment
These defects may appear to be mere cosmetic blemishes, but they are fatal to sealing—every slight protrusion or indentation can create a … on the sealing surface. Leakage channel . The user cannot see the 0.1-millimeter burr on the cup rim, But you can tell from the water.

05、 Root Cause #3: The Most Subtle Link—Tolerance Accumulation

Everything mentioned earlier still falls under issues “within one’s own control.” The real hidden challenge lies in the next one.
In the domestic general enterprise standard for disposable plastic lids, The tolerance for the inner diameter of the port is ±0.2 mm. . And in order to ensure compatibility with cup bodies from different manufacturers and different production batches, the beverage product, Manufactured with tolerances set at the upper limit. 。       

\\ ±0.2 + ±0.2

The cup body and the lid are manufactured by different companies, so the tolerances from each side add up.

The lid appears to be securely fastened, but it may not be tightly sealed in certain areas; a gentle squeeze of the cup body or pressure from the delivery bag can expose previously hidden gaps.
This explains a common dilemma: We’ve switched to several lid suppliers, but the problem persists. Because you’re adjusting the downstream tolerance, while the cup opening itself has always been at the upper limit of its tolerance.
Rather than repeatedly changing the lid, why not measure the cup’s opening first?
The following four exercises won’t cost you a thing.
✓ 1. Measure the outer diameter of the measuring cup’s opening, and take measurements from multiple directions.
Measure by rotating the dial caliper around the circumference. If the readings differ in different directions, it indicates that the cup opening has become elliptical or deformed—in which case no matter how many lids you try, they won’t fit. By the way: if the wall‑thickness deviation exceeds… ±0.2 mm That would be considered an anomaly.
✓ II. Clearance Between the Core and the Housing
The clearance between the cup lid and the cup rim, according to industry experience, is approximately 0.1–0.3 millimeters Between. Anything below this range won’t seal properly, while anything above it is prone to leakage.
✓ III. Perform an inversion test
Fill with water, screw on the lid, Place it upside down for 2 minutes. , check whether there’s any seepage around the cup rim. This is the simplest and most straightforward way to verify a seal.
✓ IV. Check the temperature log
If the cup rims in the same batch are inconsistent, check the records for the heating zone—especially the actual temperature at the zone corresponding to the cup rims—to see whether it fluctuates between batches.
In the equipment business, our perspective on these kinds of issues differs from that of those who make cups: Many people focus on the downstream process to identify the root cause, but the answer often lies in the temperature profile of the upstream process.
Ultimately, the roundness of the cup’s rim is determined in those few seconds of heating and shaping; no matter how carefully you pick a lid afterward, you’re still paying for what came before.
Whether a cup leaks or not is something users don’t bother to investigate. All they’ll remember is: that brand spilled all over me.